A curing oven that drifts a few degrees outside its setpoint, a washer pump that begins to vibrate, or an extraction fan drawing more current than usual can all signal a developing problem. Predictive maintenance sensors give facility teams visibility into those early changes, before they become an emergency shutdown, rejected batch, hygiene concern, or expensive repair.
For plants that depend on controlled heating, drying, washing, sterilization, and material handling, the objective is not to add technology for its own sake. It is to make maintenance decisions based on the actual condition of equipment. The right sensor strategy helps teams protect production schedules, improve safety, and extend the useful life of critical machinery.
What Predictive Maintenance Sensors Measure
Predictive maintenance is condition-based maintenance supported by data. Rather than servicing a machine only after it fails or following a fixed calendar interval, maintenance personnel use measured changes in performance to determine when attention is needed.
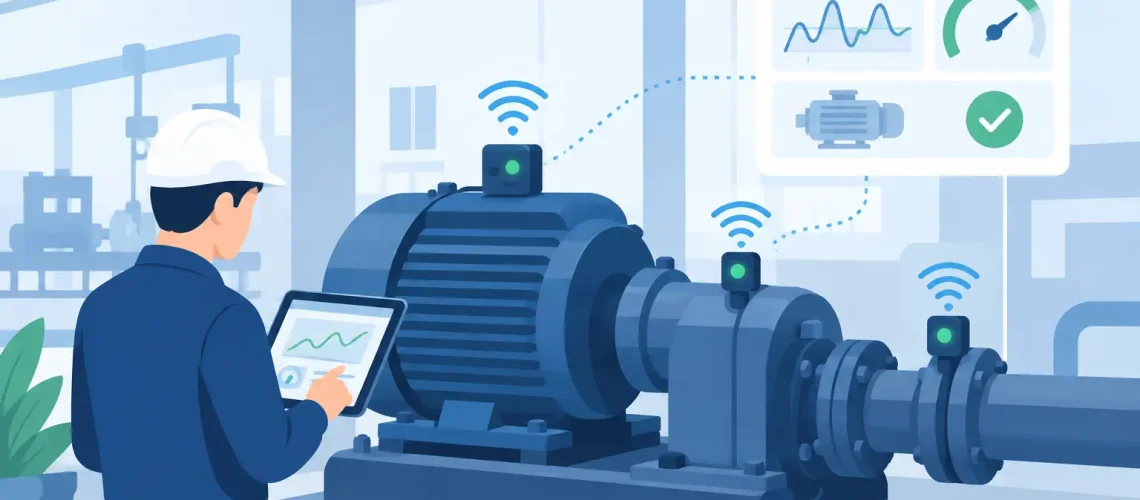
Sensors can monitor a range of mechanical, electrical, and process conditions. Vibration sensors are commonly used on motors, fans, gearboxes, bearings, and pumps. A rise in vibration at a particular frequency may indicate imbalance, misalignment, looseness, or bearing wear. Temperature sensors can identify overheating in bearings, motors, oven zones, electrical cabinets, and thermal insulation areas.
Electrical monitoring is equally valuable. Current, voltage, and power sensors can reveal a motor that is working harder than normal, a heater bank that is not performing as expected, or an electrical load that has become unstable. Pressure and flow sensors are useful in washing, spraying, drying, and ventilation systems, where a blocked line, worn pump, leaking connection, or clogged filter can affect process results.
Other applications may require humidity, dew point, particulate, door-cycle, level, or air-quality monitoring. In thermal and sanitation equipment, process sensors should not be treated separately from equipment health. A temperature deviation may point to a product-quality issue, but it may also reveal a failing heater, damaged door seal, weak airflow, or control problem.
Why Condition Monitoring Matters in Process-Critical Facilities
Unplanned maintenance is disruptive in any plant. In a facility with curing, sterilization, drying, or washing processes, the consequences can extend beyond lost operating hours. A fault can affect batch consistency, energy consumption, workplace safety, sanitation controls, and regulatory obligations.
Consider an industrial oven fan motor. If its bearing begins to degrade, the oven may still operate for weeks. However, airflow can become less consistent, the motor can draw more power, and the risk of sudden stoppage rises. Monitoring vibration and current gives the maintenance team time to inspect the motor, schedule replacement parts, and carry out work during a planned production window.
The same principle applies to a washer pump or a sterilization trolley mechanism. A small decline in pressure, cycle time, or motor performance may not stop the machine immediately. Yet it can compromise cleaning results or place additional stress on other components. Early intervention is generally less costly than responding after a failure has damaged a pump, contaminated a process, or delayed a customer delivery.
Predictive monitoring also supports more disciplined energy management. Equipment that operates outside its normal electrical or thermal profile often consumes more energy. Identifying those changes can help facilities correct the cause rather than accepting higher utility costs as unavoidable.
Selecting Sensors for the Equipment You Actually Operate
The most effective program starts with the equipment, its failure modes, and the operational consequences of failure. A sensor package should be selected because it answers a useful maintenance question, not because it produces the largest volume of data.
Begin by identifying critical assets. These are usually machines that create a production bottleneck, have long replacement lead times, present a safety risk, or directly affect product hygiene and quality. An exhaust fan serving a curing oven, for example, may be more critical than a small auxiliary motor that can be replaced quickly.
Next, consider how each asset is likely to fail. Rotating equipment often benefits from vibration and temperature measurement. Heater systems may require temperature feedback, current monitoring, and contactor or relay inspection. Pumps can be monitored through pressure, flow, vibration, and motor load. Electrical control panels may require temperature, power quality, and cabinet-environment monitoring.
Sensor placement matters as much as sensor type. A vibration sensor mounted on a motor housing can provide meaningful bearing data, while one installed on a flexible guard may not. A temperature probe placed too far from the area of concern can mask an overheating component. Installation should account for access, cable routing, washdown exposure, electromagnetic interference, and the operating temperature of the equipment.
Wireless sensors can reduce installation work and suit difficult-to-reach locations. Wired sensors may be the better choice where continuous monitoring, high sampling rates, or stable communication is essential. Neither approach is automatically superior. The right decision depends on the machine, plant environment, network capability, and maintenance objective.
Data Is Useful Only When It Leads to Action
A common mistake is collecting readings without defining who will review them, what constitutes an alert, and how the team should respond. A maintenance program becomes effective when sensor data is connected to clear operating limits and practical work processes.
For each monitored asset, establish a normal baseline. This should reflect real operating conditions, including production load, ambient temperature, and cycle requirements. A fan operating at full heat load may naturally show different vibration and current values than it does during idle operation. Comparing unlike conditions can create false alarms and waste maintenance time.
Alert thresholds should be set in stages. A warning may trigger a planned inspection, while a critical alert may require immediate action or controlled shutdown. The thresholds should be reviewed after the team has gathered enough operating history. Manufacturer specifications provide a starting point, but the equipment’s own performance trend is often the most useful reference.
Data should feed into the maintenance workflow, whether that is a computerized maintenance management system, a plant dashboard, or a structured review process. If an alert appears, the team needs a defined response: verify the reading, inspect the machine, document findings, and schedule corrective work. Sensor data does not replace experienced technicians. It helps them focus their time where it has the greatest value.
The Trade-Offs to Plan For
Predictive maintenance sensors require investment in hardware, installation, data handling, training, and ongoing review. They are most valuable on critical or failure-prone equipment. Applying extensive monitoring to every low-cost asset can create complexity without delivering a proportionate return.
There is also a difference between detecting a condition and diagnosing its cause. A high-temperature alert may indicate bearing friction, poor lubrication, excess electrical load, inadequate cooling, or an inaccurate sensor. Teams still need sound engineering judgment and inspection procedures to determine the right corrective action.
Environmental suitability is another practical consideration. Sensors installed near ovens, spray booths, wash areas, or sterilization processes must tolerate heat, moisture, chemicals, vibration, and cleaning routines. The enclosure rating, cable protection, mounting method, and calibration requirements should be specified as part of the machinery design or retrofit scope.
Cybersecurity and network ownership should also be addressed early, particularly where sensor systems communicate with plant controls or cloud-based platforms. Facilities need clarity on data access, user permissions, system updates, and what happens if communication is interrupted. Monitoring should support operations without creating a new source of risk.
Building a Practical Monitoring Program
A sensible first project is usually a pilot on a small number of high-value assets. Select equipment with a known maintenance history, measurable failure patterns, and a clear operational impact. Track whether the monitoring program reduces emergency callouts, improves planned maintenance completion, lowers spare-parts urgency, or prevents process interruptions.
Use the pilot to refine alarm settings and maintenance responses before expanding coverage. It is also an opportunity to involve operators, who often notice changes in sound, cycle behavior, and machine response before any dashboard does. Their observations add valuable context to the sensor record.
For custom-built process equipment, predictive monitoring is most effective when considered during design. REK Engineering Machinery can incorporate appropriate sensing, control-panel integration, and service access into equipment built for specific thermal, hygiene, and industrial workflows. For existing machinery, a site assessment can identify where retrofit monitoring will provide the strongest return.
The goal is not a control room filled with alarms. It is a maintenance team that can see developing issues early enough to make calm, informed decisions. Start with the assets that matter most, establish useful baselines, and make every alert lead to a clear next step.