A sanitation failure in pharmaceutical production rarely stays contained. A poorly cleaned transfer cart, an improperly dried washer, or an uncontrolled personnel entry point can introduce residues, microbes, or particles into a process that depends on repeatability. These pharmaceutical sanitation examples show how facilities turn hygiene requirements into controlled, verifiable daily operations.
For pharmaceutical plants, sanitation is not a single cleaning task performed at the end of a shift. It is a coordinated system of equipment design, documented procedures, trained personnel, validated cycles, and maintenance. The required level depends on the product, process area, and applicable quality requirements. A non-sterile solid-dose line has different controls than an aseptic filling suite, but both need disciplined sanitation practices.
Pharmaceutical Sanitation Examples Across the Facility
1. Cleanroom entry and gowning control
Personnel are a major source of particles and microbial contamination. Controlled entry begins with a defined change sequence: removing unsuitable personal items, washing hands, putting on required garments in the correct order, and entering through an airlock or controlled transition area.
The physical layout matters as much as the written procedure. Benches that separate clean and less-clean sides, hands-free sinks, garment storage, and clearly marked personnel flow reduce opportunities for cross-contamination. For higher-grade rooms, facilities may also use air showers or pressure-controlled entry areas. The best arrangement is the one operators can follow correctly every time, even during busy shift changes.
2. Sanitizing work surfaces between batches
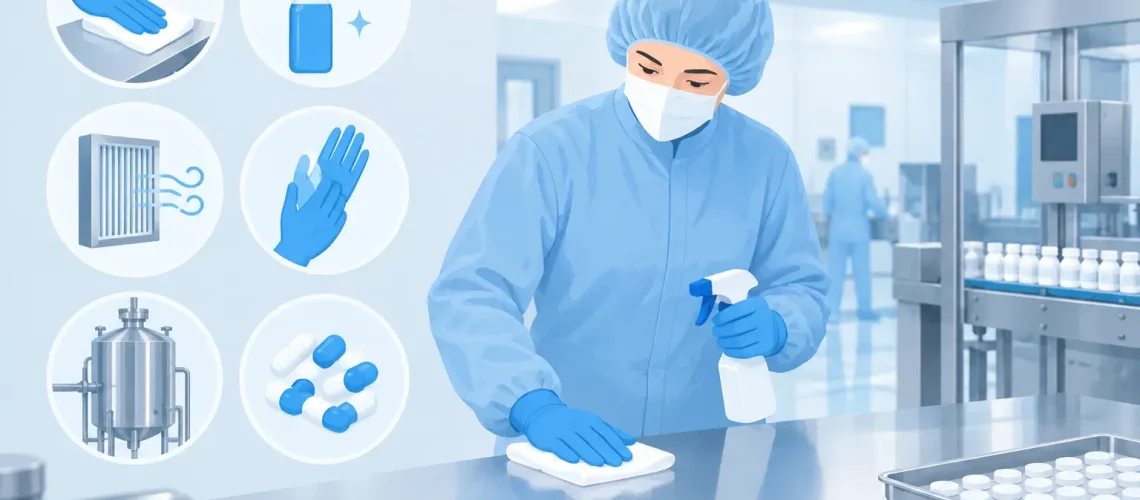
Benchtops, control panels, doors, chairs, and staging areas must be cleaned according to a defined frequency and method. A typical program specifies the approved detergent or disinfectant, concentration, contact time, wiping technique, and rotation schedule for disinfectants where appropriate.
This is not simply spraying and wiping until a surface looks clean. Operators should remove visible soil first, apply the solution at the required wet-contact time, and use clean wipes in a pattern that avoids transferring contamination back onto sanitized surfaces. Records should identify the area, date, chemical lot, and operator. These details support traceability when an investigation is required.
3. Clean-in-place for tanks and process piping
Clean-in-place, or CIP, is one of the most practical pharmaceutical sanitation examples for enclosed process equipment. Product vessels, transfer lines, pumps, and pipework can be cleaned without dismantling every component. A programmed cycle may include pre-rinsing, detergent washing, intermediate rinsing, final rinsing, and drying or sanitization as required by the process.
CIP performance depends on more than cycle duration. Flow rate, temperature, chemical concentration, spray coverage, drainability, and pipe geometry all affect results. Dead legs, poorly positioned spray devices, and incomplete drainage can leave residues that threaten product quality. Facilities should use conductivity, temperature, time, flow, and other suitable process data to confirm each cycle has operated within its established parameters.
4. Washing removable parts and utensils
Not every item can remain in a closed system. Change parts, containers, scoops, trays, tools, and small machine components often require manual cleaning or automated washing. An industrial washer provides greater consistency where the load type, spray pattern, water pressure, and drying conditions can be controlled.
A sound workflow separates dirty receiving, washing, drying, inspection, and clean storage. Cleaned parts should not travel back through an unclean area before use. Equipment selection should reflect the size and complexity of the load. A small parts washer may be effective for fittings and utensils, while trolleys, racks, and larger assemblies require a chamber that delivers adequate coverage and drainage.
5. Drying after washing
Drying is sometimes treated as an afterthought, yet retained moisture can support microbial growth, cause corrosion, or compromise clean storage. Pharmaceutical facilities may use filtered hot-air drying cabinets, dedicated drying rooms, or washer-dryers that complete the wash and dry sequence in one controlled system.
The right temperature is product- and material-dependent. Excessive heat can damage seals, plastics, labels, or sensitive components; insufficient heat or airflow leaves moisture in crevices. Drying equipment should provide predictable air circulation and allow operators to verify that loads are dry before release. This is especially relevant for stainless-steel vessels, reusable garments, and equipment parts that return to controlled production zones.
6. Trolley and material transfer sanitation
Carts and trolleys regularly cross boundaries between warehouses, wash areas, production rooms, and waste handling points. Their wheels, handles, shelves, and lower frames can carry contamination into cleaner areas if they are not included in the sanitation plan.
A dedicated trolley washer or sterilizer can standardize treatment for high-use transfer equipment. Facilities may also establish separate trolleys by area classification, with color coding or identification to prevent mix-ups. The right approach depends on material flow, area classification, and whether the trolley contacts exposed product components. What matters is that the transfer route is engineered and documented rather than assumed to be clean.
7. Controlled sanitation of filling and packaging equipment
Filling nozzles, hoppers, conveyor guides, blister packaging contact parts, and bottle handling equipment require particular attention because contamination at this stage can directly affect finished product quality. Some lines need disassembly and manual cleaning between campaigns; others use automated cleaning cycles or removable assemblies sent to a washer.
Sanitation procedures should identify difficult-to-clean locations, including seals, threads, guards, underside surfaces, and interfaces where product can accumulate. Visual inspection is useful but not enough for critical equipment. Depending on the process, facilities may use rinse sampling, swab testing, or other validated verification methods to demonstrate that cleaning has met acceptance criteria.
8. Hand hygiene and high-touch point control
Hands, door handles, touchscreens, telephones, shared tools, and push plates are frequent contact points. Handwashing stations should be positioned where personnel need them, stocked consistently, and designed to avoid recontaminating clean hands. Hands-free faucets, dispensers, and waste bins reduce unnecessary touchpoints.
High-touch surfaces should appear in the routine sanitation schedule, not only in response to an incident. The frequency should be based on traffic, room function, and risk. In a controlled manufacturing environment, a practical schedule that teams can consistently complete is stronger than an overly complicated program that gets skipped when production demand rises.
9. Waste handling and dirty-side segregation
Waste is part of the sanitation system. Used wipes, rejected materials, damaged containers, and process residues must move out of controlled areas without crossing clean material routes. Covered, clearly labeled waste containers and defined removal times help prevent accumulation.
For facilities handling potent compounds or biologically active materials, containment and decontamination requirements may be more demanding. The waste route, cleaning tools, protective equipment, and holding areas should be assessed as one process. A cleanroom can be well maintained, but poor waste movement can undermine its controls within minutes.
10. Sanitizing reusable textiles and protective garments
Reusable cleanroom garments, protective clothing, and facility textiles require controlled laundering, drying, and storage. The objective is not merely to remove visible staining. The wash cycle must reliably remove residues and reduce contamination while protecting the textile’s filtration and barrier properties.
Industrial laundry systems can provide repeatable wash temperatures, chemical dosing, extraction, and drying. Segregation is essential: soiled garments must remain separate from cleaned garments, and clean items need protected storage before distribution. REK Engineering Machinery supports hygiene-focused facilities with custom washing, drying, and trolley sanitation equipment designed around actual load sizes, handling routes, and operating requirements.
What Makes a Sanitation Example Effective?
An effective sanitation practice has three characteristics: it is repeatable, measurable, and workable for the people who perform it. A procedure that depends on individual judgment alone will vary from shift to shift. A system with defined parameters, suitable machinery, clear work instructions, and inspection points gives operators a reliable standard.
Validation and verification serve different purposes. Validation establishes evidence that a process can consistently achieve its intended result. Verification confirms that the approved process was actually followed and remains in control. For example, a washer cycle may be validated for a specific load configuration, while each operating cycle is verified through recorded time, temperature, pressure, and chemical-use parameters.
Equipment maintainability is also a sanitation decision. Smooth, drainable surfaces, accessible service points, corrosion-resistant materials, and simple controls reduce the chance that hygiene performance will deteriorate over time. Preventive maintenance should cover worn seals, blocked spray nozzles, damaged door gaskets, sensor accuracy, drainage, and airflow performance. A machine that once cleaned effectively can become a sanitation risk when maintenance is deferred.
The strongest pharmaceutical sanitation programs are built around the real movement of people, materials, equipment, and waste through a facility. Start by following those routes on the plant floor, identify where contamination could be carried forward, and design controls that operators can sustain with confidence.