A curing chamber that is too small becomes the production bottleneck. One that is too large costs more to build, takes longer to stabilize, and may waste energy on every cycle. Knowing how to size curing chambers starts with a clear view of the product, the coating or material specification, and the production schedule the equipment must support.
For industrial coating, powder curing, adhesive bonding, composite processing, and similar thermal applications, chamber size is not simply a matter of choosing a length, width, and height. It is an engineering decision that connects loading methods, airflow, heat transfer, cure time, operator access, safety clearances, and future capacity. The right design delivers repeatable results without forcing a facility to compromise its workflow.
Start With the Required Production Throughput
The first sizing question is not, “How large is the part?” It is, “How much finished product must leave the process each hour or shift?” Establish the required throughput in units, racks, batches, or total product weight. Then account for the actual production pattern. A line producing 80 parts evenly across an eight-hour shift has different equipment needs than a line that must cure all 80 parts in two concentrated production windows.
For a batch chamber, calculate the number of loads required per shift. Divide the available operating time by the complete cycle time, not only the dwell time at curing temperature. A complete cycle can include loading, door closing, heat-up, temperature recovery after loading, the specified cure hold, cooling if it occurs in the chamber, unloading, and any required cleaning or inspection.
For example, a coating requires a 25-minute cure after the product reaches metal temperature. The chamber may need another 20 minutes for loading, heat-up, recovery, unloading, and handling. Its realistic cycle is therefore 45 minutes, not 25 minutes. If the facility needs 10 full loads per shift, one chamber may be adequate only if the shift length, planned breaks, and allowance for normal delays support that schedule.
Conveyorized chambers use the same principle, but the calculation begins with line speed and product pitch. If parts are suspended 24 inches apart and the required time in the heated zone is 30 minutes, conveyor speed and heated length must work together to provide that residence time. Changes to spacing, carrier design, or throughput can affect the required chamber length significantly.
Define the Usable Load Envelope
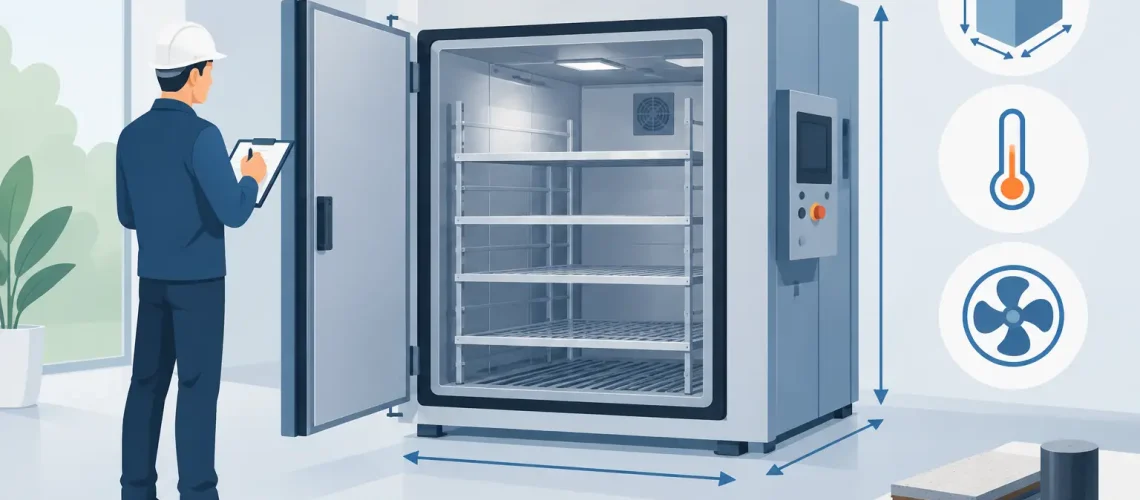
External chamber dimensions are not usable curing dimensions. The load envelope must allow room for racks, trolleys, fixtures, conveyors, product movement, air circulation, and safe loading access. Start by documenting the maximum product dimensions, but do not size the chamber around a single ideal part unless that part represents the normal production mix.
A practical load study should include the widest, tallest, longest, and heaviest products expected to run, along with the typical product. Consider whether parts will be loaded on wheeled trolleys, fixed shelves, hanging racks, pallets, or custom fixtures. Each method changes the usable volume and influences how heated air can reach the workpiece.
Clearance matters. Products positioned too close to walls, heaters, ducts, or adjacent parts may receive uneven airflow and inconsistent heat transfer. Large flat panels, deep cavities, dense assemblies, and tightly packed racks are especially sensitive. A chamber may physically fit the load yet still fail to cure it uniformly if air cannot circulate around critical surfaces.
Door openings deserve equal attention. The chamber opening must accommodate the trolley or product at its widest point, including handles, guide rails, and safe operator clearance. A chamber with a generous internal volume but an undersized doorway creates an expensive operational problem.
Allow for the Future Product Mix
It is reasonable to build some growth allowance into a custom curing chamber, but oversizing without a production basis can reduce operating efficiency. The better approach is to identify likely future products, anticipated rack changes, and growth targets over the next three to five years. If expansion is probable, a modular chamber arrangement, additional trolley positions, or controls designed for future zones may be more effective than installing excess heated volume on day one.
Calculate the Real Thermal Load
Chamber volume alone does not determine heater capacity. The equipment must heat the product, its fixtures, racks, trolleys, and the air inside the chamber while overcoming heat loss through walls, doors, exhaust, and openings. In many applications, the product and fixture mass drive the heat-up requirement more than the air volume.
The thermal calculation should consider the total mass entering at ambient temperature, the target cure temperature, the desired ramp time, and the material heat capacity. A heavy steel fabrication on a substantial trolley requires much more energy than a lightweight aluminum part, even if both occupy the same physical space. Dense loads may also heat slowly at their center, which can extend the time required for all surfaces to reach the specified curing temperature.
Heat loss must be assessed at steady state as well. Insulation thickness and construction quality influence energy use, outer-surface temperature, and the chamber’s ability to hold its setpoint under production conditions. Door openings, fresh-air requirements, and exhaust systems add further demand. Where coatings release solvents or other volatiles, engineered ventilation and safety controls are necessary, and these requirements directly affect heating capacity.
A sound design separates two questions: how much power is needed to reach temperature within the required time, and how much power is needed to maintain temperature during normal operation. Sizing only for steady-state operation can produce slow recovery after loading. Sizing only for rapid heat-up can add unnecessary capital and demand charges. The correct balance depends on the cycle schedule and process tolerance.
Size Airflow for Temperature Uniformity
Curing performance is governed by the temperature at the product, not merely the temperature shown on the chamber controller. Airflow distribution determines whether heat reaches all parts of the load evenly, particularly where products have varying mass, complex shapes, or shadowed surfaces.
A well-designed forced-air system uses fans, ducting, baffles, and return paths to move heated air through and around the load. Fan capacity must suit the chamber volume and load density, but high airflow alone is not the answer. Excessive velocity can disturb lightweight components or create uneven patterns if the supply and return arrangement is poorly planned. Insufficient airflow can leave cold zones and lengthen recovery times.
This is where standard chamber dimensions often fall short. A rack of small open components behaves very differently from a trolley holding enclosed cabinets, heavy automotive parts, or densely arranged fabricated assemblies. Custom airflow modeling and practical load trials help establish the right duct placement, fan arrangement, and rack spacing for the actual process.
Confirm the Cure Specification
Before finalizing chamber size, review the coating, adhesive, resin, or material supplier’s cure schedule. Specifications may state a required air temperature, a product temperature, or a time at product temperature. These are not interchangeable. If a specification calls for 20 minutes at 350°F metal temperature, the process must account for the time required for the coldest point of the product to reach 350°F.
Temperature mapping and product-temperature testing are valuable during commissioning. Multiple sensors placed around the working zone can verify chamber uniformity, while thermocouples on representative product locations confirm that the curing profile is achieved. This evidence supports consistent quality, process documentation, and confident troubleshooting later.
Plan the Chamber Around Facility Operations
The curing chamber must work within the plant, not just on a layout drawing. Review floor space, ceiling height, floor loading, access routes, electrical supply, fuel source where applicable, ventilation, fire protection, and maintenance access. A chamber can be correctly sized for production but still create disruption if operators cannot stage loads safely or service personnel cannot access fans, heaters, sensors, and control panels.
Material flow is equally important. Ideally, incoming work, loading, curing, unloading, cooling, inspection, and packing follow a logical path without unnecessary crossing traffic. In a powder coating operation, for example, the distance between spray booth, flash-off area, curing chamber, and cooling zone affects both labor efficiency and finish quality.
Controls should match the process complexity. At minimum, operators need clear temperature indication, programmable recipes where multiple products are processed, over-temperature protection, alarms, and appropriate interlocks. Facilities with traceability requirements may also need cycle records, temperature logging, user access control, or integration with plant systems.
Choose a Sizing Method That Reflects Reality
The most reliable way to size a curing chamber is to base the design on documented production data and representative loads. Provide the equipment engineer with product drawings, material weights, fixture details, target throughput, cure profiles, available utilities, and layout constraints. If the product mix is broad, identify the loads that are most thermally demanding and most common, rather than relying on an average that may not represent either case.
A competent engineering review should test the trade-offs openly. A larger load capacity may reduce the number of cycles but require more handling time. Faster heat-up may improve throughput but increase connected electrical load. Higher airflow may improve uniformity for one product while requiring revised fixturing for another. These are process choices, not details to resolve after installation.
REK Engineering Machinery approaches curing equipment as part of the wider production system, with chamber construction, controls, airflow, loading arrangements, installation, and ongoing service considered together. That approach helps facilities avoid the common mistake of buying a chamber that looks adequate on paper but cannot perform reliably under shift conditions.
The best chamber size is the one that gives your operators enough working room, gives every product the required thermal profile, and leaves your production schedule with breathing room. Start with the load and the cure requirement, then let the engineering follow.