A curing oven set 10°F too low can leave a coating under-cured. A sterilizer reading 5°F too high can create a more serious problem: a cycle that appears compliant while missing its required thermal conditions. Knowing how to calibrate thermal sensors is therefore not simply a maintenance task. It is a practical control measure for product quality, hygiene, safety, energy use, and traceable process performance.
Thermal sensors are found throughout industrial ovens, furnaces, dryers, washers, heat-treatment equipment, and sterilization systems. Their readings drive heaters, alarms, recorders, and automated cycle decisions. When the sensor, wiring, controller, or installation method introduces error, operators may see stable numbers on the display without having stable conditions inside the machine.
Start With the Process Requirement
Calibration begins by defining what the temperature measurement must achieve. A drying process may tolerate a small deviation, while food processing, healthcare sanitation, electronics curing, or aerospace heat treatment may require tighter control and documented evidence. The acceptable tolerance should come from the product specification, applicable regulation, customer requirement, or validated process procedure.
Also distinguish between sensor calibration and system verification. A sensor can agree with a reference thermometer when tested by itself, yet the installed system may still read incorrectly because of heat transfer, sensor location, controller scaling, damaged extension wire, or electrical interference. For process-critical equipment, verify the complete measurement chain.
Before starting work, review the equipment manual, prior calibration records, alarm limits, sensor type, and operating temperature range. Confirm whether the machine uses a thermocouple, resistance temperature detector (RTD), thermistor, infrared sensor, or another measurement technology. Each requires a different test approach and has different common failure modes.
How to Calibrate Thermal Sensors Step by Step
1. Use a traceable reference standard
The reference instrument must be more accurate than the device under test. A common practice is to use a reference with accuracy at least four times better than the required process tolerance, although the appropriate ratio depends on the uncertainty of the application.
For contact sensors, use a certified reference thermometer with a suitable probe, dry-block calibrator, temperature bath, or controlled calibration furnace. The selected standard must cover the operating range and have current traceable calibration documentation. A kitchen thermometer or an unverified handheld meter is not an acceptable reference for industrial process control.
For non-contact infrared sensors, use a calibrated blackbody source. Surface finish, emissivity, distance, viewing angle, and reflected energy all affect infrared readings, so an ice bath or dry block is not an equivalent test method.
2. Inspect the sensor and its installation
Before comparing readings, inspect the full assembly. Look for crushed leads, loose terminals, corroded connectors, moisture entry, worn insulation, bent probes, damaged protective sheaths, and signs of overheating. On thermocouples, confirm that the extension cable matches the thermocouple type. Using incorrect compensating cable can produce a meaningful error even when the probe itself is functional.
Check the installation location as well. A probe placed too close to a heating element, wall, steam inlet, fan discharge, or cold air leak may measure a local condition instead of the actual product environment. In forced-air ovens and dryers, airflow can make temperature vary significantly between the sensor location and the load area.
3. Stabilize at multiple test points
Calibrate across the range that matters to the process, not only at one convenient temperature. For an oven normally operated between 250°F and 450°F, tests near the low, normal, and high operating points provide a more useful result than a single check at room temperature.
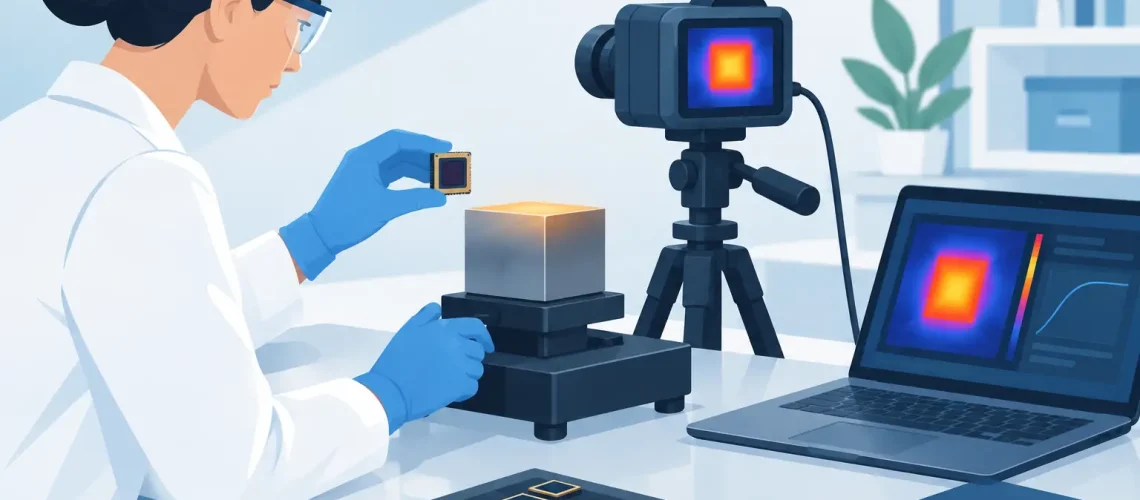
Place the reference probe and the sensor under test as close together as possible in the same stable temperature zone. Allow enough time for both instruments to reach equilibrium. This is where rushed work often creates false results. A probe with a heavy stainless-steel sheath may take several minutes longer to stabilize than a fine-wire thermocouple.
Record the reference value, indicated value, deviation, test-point time, equipment identification, reference-standard identification, and ambient conditions where relevant. Repeat readings if the values are unstable. Fluctuation may point to a control issue, airflow problem, poor sensor contact, or failing electrical connection rather than a simple calibration offset.
4. Adjust only when the system permits it
Some transmitters, controllers, and digital indicators allow an offset adjustment. If adjustment is authorized, apply only the correction supported by the test results and then repeat the measurement at every test point. Do not adjust a controller merely to make one point look correct if doing so causes unacceptable error elsewhere in the range.
Many sensors, especially thermocouples and RTDs, cannot be meaningfully adjusted at the sensor itself. When the sensor has drifted beyond tolerance, replacement is usually the correct action. Attempts to compensate for severe drift through controller offsets can hide an aging sensor and complicate future troubleshooting.
After any adjustment or replacement, confirm alarm and shutdown functions. A high-temperature alarm that activates at the wrong value can damage product, waste energy, or expose personnel and equipment to avoidable risk.
5. Verify the process, not only the display
A controller display may match the reference probe while the working chamber still contains hot and cold areas. For ovens, furnaces, dryers, washers, and sterilizers, conduct temperature mapping or heat-distribution testing when the process requires uniform conditions. This involves placing multiple calibrated sensors throughout the usable work zone and recording temperatures through a representative cycle.
The test should reflect actual production conditions. An empty oven can perform differently from one loaded with heavy metal parts, textile goods, medical carts, or packaged products. Load mass, airflow restriction, door openings, humidity, conveyor speed, and rack position can all affect achieved temperature.
Common Sources of Calibration Error
Sensor drift is a normal concern in high-temperature or chemically demanding service. Thermocouples can drift due to oxidation, contamination, vibration, and prolonged exposure to heat. RTDs may shift after mechanical damage or moisture intrusion. Infrared sensors can produce misleading readings when lenses are dirty or emissivity settings do not match the target material.
Cold-junction compensation is another frequent issue with thermocouple systems. The instrument must accurately account for the temperature at the connection point. Loose terminals, unsuitable connectors, and excessive heat around the control panel can influence this compensation.
Do not overlook the controller configuration. A system may be programmed for the wrong sensor type, temperature unit, input range, or scaling value. For example, a Type K thermocouple connected to an input configured for Type J will produce readings that may appear plausible while becoming increasingly inaccurate across the range.
Set a Calibration Interval Based on Risk
There is no universal interval for thermal sensor calibration. A sensor used daily in a 1,200°F furnace needs closer attention than one used occasionally in a low-temperature storage room. The right interval depends on process criticality, operating temperature, sensor technology, environmental exposure, usage frequency, historical drift, and the consequences of an out-of-tolerance condition.
For critical equipment, establish an interval from documented risk and performance data. Review calibration results over time. If readings repeatedly remain well within tolerance, an interval may be extended with appropriate approval. If sensors show frequent drift, unexplained failures, or exposure to harsh conditions, shorten the interval and investigate the underlying cause.
A practical program also includes checks after maintenance, power events, sensor replacement, controller replacement, or a suspected process deviation. Calibration certificates alone do not protect the process if changes occur between scheduled service dates.
Document Results for Reliable Operations
A useful calibration record identifies the equipment and sensor, the method used, reference-standard details, test points, as-found readings, adjustments made, as-left readings, acceptance criteria, date, technician, and next due date. If a sensor is found out of tolerance, document the impact assessment. Determine which batches, cycles, or sanitation loads may have been affected since the last acceptable verification.
This documentation supports internal quality control, customer audits, preventive maintenance planning, and regulatory-conscious operations. More importantly, it gives plant teams a clear basis for action rather than relying on assumptions about what the display says.
For custom thermal equipment, calibration should be considered during machine design as well as maintenance. Accessible sensor locations, stable airflow, correctly selected probes, properly routed cabling, and control panels configured for the application make future verification faster and more dependable. REK Engineering approaches these details as part of long-term equipment performance, not as an afterthought after installation.
A well-calibrated sensor is valuable because it gives operators confidence to act on the temperature they see. Build that confidence with suitable standards, realistic process testing, disciplined records, and service support that treats every thermal reading as a decision point for quality and safety.